Aluminum Sheet Metal Fabrication: Alloys, Bending, Welding and Finishes
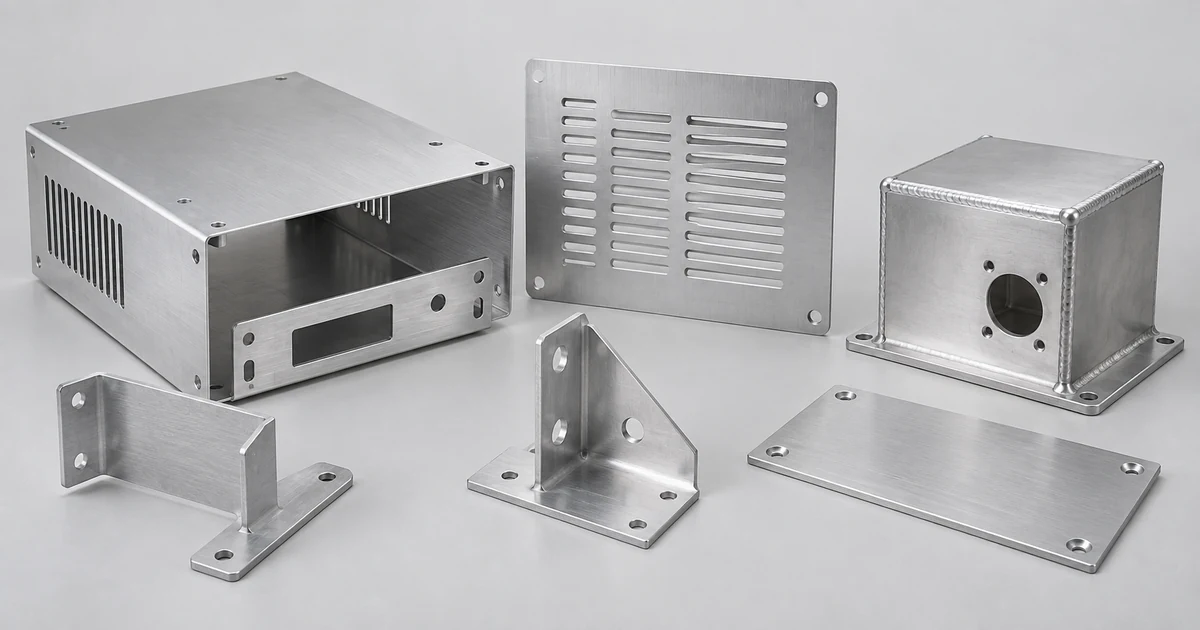
Aluminum sheet metal fabrication turns flat aluminum stock into lightweight enclosures, brackets, panels, chassis and welded assemblies. A reliable result depends on more than choosing “aluminum.” The alloy, temper, thickness, grain direction, bend radius, joining method and finish must work together.
What Is Aluminum Sheet Metal Fabrication?
Aluminum sheet metal fabrication is a sequence of manufacturing operations used to convert flat sheet into a finished component. A typical workflow includes blanking or laser cutting, punching, deburring, press-brake bending, hardware installation, welding or mechanical assembly, surface finishing and dimensional inspection.
The process is well suited to parts that need low weight, corrosion resistance, electrical or thermal performance, and a clean appearance. Common examples include electronics housings, instrument panels, vehicle brackets, battery enclosures, guards, covers, trays and laboratory equipment.
However, aluminum behaves differently from mild steel. It has a lower elastic modulus, transfers heat quickly and can show cosmetic marks easily. As a result, the drawing and process plan should address stiffness, springback, bend radii, welding distortion, surface protection and handling from the beginning.
Common Aluminum Alloys for Sheet Metal Fabrication
Alloy and temper are separate decisions. The alloy identifies the chemical composition family, while the temper describes the mechanical or thermal treatment condition. Both affect strength, formability, welding and appearance.
| Alloy and temper | Fabrication characteristics | Typical applications |
|---|---|---|
| 5052-H32 | Good corrosion resistance, reliable formability and good weldability. Often preferred for parts with multiple bends. | Enclosures, brackets, covers, panels, trays and marine-related parts. |
| 6061-T6 | Higher strength and good machinability. Weldable, but tight bending is less forgiving than with 5052-H32. | Structural brackets, frames, fixtures and combined machined/fabricated parts. |
| 3003-H14 | Very good formability and useful general corrosion resistance, with lower strength than 5052 or 6061. | Ducting, covers, decorative panels, light-duty housings and formed components. |
| 5754-H22 | Good forming, welding and corrosion performance. Frequently considered for transportation and outdoor assemblies. | Automotive panels, guards, tanks, enclosures and marine components. |
| 5005-H34 | Useful for decorative sheet applications and consistent anodized appearance when material control is important. | Architectural panels, trim, covers and appearance-sensitive products. |
Aluminum Sheet Thickness and Gauge
Aluminum gauge numbers do not match steel gauge numbers. For example, 16-gauge aluminum is approximately 0.0508 in (1.290 mm), while 16-gauge mild steel is approximately 0.0598 in (1.519 mm). The safest production drawing specifies the alloy, temper and nominal thickness in inches or millimeters.
Use the sheet metal thickness chart to compare common aluminum, steel and stainless steel gauge values. For a quotation, include the numerical thickness even if a gauge number is also shown.
Cutting and Punching Aluminum Sheet
Laser cutting
Modern fiber laser systems can produce detailed aluminum profiles, ventilation patterns, slots and small holes. The machine setup must account for aluminum’s reflectivity and thermal conductivity. Cut quality depends on alloy, thickness, assist gas, focus, speed and protective-film condition.
Waterjet cutting
Waterjet cutting avoids a heat-affected zone and can process thicker stock or parts that are sensitive to thermal input. It may be selected when edge condition, material thickness or downstream requirements make thermal cutting less attractive.
CNC punching and shearing
Punching is efficient for repeated holes, louvers, knockouts and formed features, especially at production quantities. Shearing is economical for straight blanks. Both processes require allowances for burr direction, edge condition and later bending.
Regardless of the cutting method, deburring should be defined. Small burrs can interfere with assembly, coating, electrical contact, sealing and safe handling.
Bending Aluminum Sheet Metal
Successful bending begins with the correct alloy and temper. A ductile alloy such as 5052-H32 generally accepts tighter bends than 6061-T6 at the same thickness. Exact limits depend on material certification, thickness, grain direction, tooling, bend angle and edge condition.
Use a realistic inside bend radius
An inside radius that is too small can produce surface tearing or cracking. Increasing the radius and orienting critical bends appropriately relative to the rolling direction can improve reliability. Appearance-critical bends may also need protective tooling or removable film.
Allow for springback
Aluminum often springs back after the forming load is removed. The bend program and tooling compensate for this behavior. A drawing should identify truly critical angles and avoid applying tight tolerances to every bend when the assembly does not require them.
Protect nearby features
Holes and slots placed close to a bend can stretch or become oval. Bend reliefs, practical edge distances and a consistent flat pattern help prevent distortion. The manufacturer should review these features before production tooling or nesting is finalized.
Welding and Assembly Methods
Aluminum sheet metal assemblies can use TIG welding, MIG welding, riveting, clinch hardware, threaded inserts, screws or structural adhesive. The correct method depends on strength, access, appearance, service temperature, conductivity and whether the assembly must be removable.
Welding requires clean material and controlled preparation because the surface oxide melts at a much higher temperature than the base aluminum. The welding plan should also consider distortion and the reduction in strength that can occur in the heat-affected zone of heat-treated alloys.
Mechanical fastening avoids welding heat and can simplify mixed-material assemblies. Captive nuts, self-clinching hardware and rivet nuts need suitable sheet thickness, hole size and edge distance. Hardware type and installation side should be marked clearly on the drawing.
Surface Finishes for Fabricated Aluminum Parts
| Finish | Main purpose | Design considerations |
|---|---|---|
| As-fabricated / mill finish | Lowest processing cost for functional parts. | Tooling marks, grain variation and light handling marks may remain. |
| Brushing | Creates a directional cosmetic texture. | Specify the grain direction and identify the visible surfaces. |
| Anodizing | Improves surface durability, appearance and corrosion performance. | Alloy, temper, welds and surface preparation can affect color consistency. |
| Powder coating | Provides color, coverage and environmental protection. | Allow for coating buildup and define masking, grounding and cosmetic zones. |
| Bead blasting | Produces a uniform matte texture before use or anodizing. | Process consistently across mating or appearance-critical parts. |
| Chemical conversion coating | Supports corrosion protection and paint adhesion while retaining conductivity options. | Specify the required chemistry, electrical contact areas and masking. |
Cosmetic requirements should be measurable. Mark Class A surfaces, acceptable grain direction, color range, maximum defect size and packaging requirements. Statements such as “perfect finish” are difficult to inspect consistently.
Tolerances and Inspection
There is no single tolerance that applies to every aluminum sheet metal part. Capability changes with part size, number of bends, distance between features, welding, material thickness and datum strategy. Flat patterns can be cut precisely, but forming and welding introduce additional variation.
Use tighter tolerances only on features that control fit or function. Define practical datums, inspection conditions and whether dimensions apply before or after coating. For welded assemblies, separate local feature requirements from overall envelope requirements when possible.
Material specifications and dimensional tolerances should be aligned with the applicable product standard. ASTM B209/B209M covers aluminum and aluminum-alloy sheet and plate, while the Aluminum Association maintains alloy, temper and product standards used across the industry.
What Affects Aluminum Sheet Metal Fabrication Cost?
The largest cost drivers are material grade, stock thickness, sheet utilization, cutting time, bend count, setup, welding, hardware, finish, inspection and quantity. Complex cosmetic requirements can add handling, surface preparation and individual packaging.
A part may cost less when it uses a readily available alloy and thickness, common tooling, accessible bends and a finish that matches its function. Combining several brackets into one complicated formed part is not always cheaper; the additional bends and tight tolerances may outweigh the saved hardware.
For a broader estimating model, review the guide to sheet metal fabrication cost. Cost comparisons should use the same material, finish, inspection level and quantity.
Design Checklist Before Requesting a Quote
- Identify the aluminum alloy and temper, not only “aluminum.”
- State nominal thickness in inches or millimeters.
- Provide both a 3D CAD model and a controlled 2D drawing.
- Mark critical dimensions, datums and inspection requirements.
- Use realistic bend radii and add relief near corners where needed.
- Define hardware type, installation side and required pull or torque performance.
- Identify weld locations, cosmetic weld requirements and acceptable distortion.
- Specify finish, color, texture, masking and visible surfaces.
- Include quantity, delivery target and packaging requirements.
These details help the engineering team review manufacturability and prepare a project-specific quotation through Xproto’s custom sheet metal fabrication service.
Häufig gestellte Fragen
What is the best aluminum alloy for sheet metal bending?
5052-H32 is a common choice for bent sheet metal parts because it offers good formability, corrosion resistance and weldability. The best alloy still depends on strength, environment, finish and stock availability.
Can 6061-T6 aluminum sheet be bent?
Yes, but 6061-T6 is less forgiving than 5052-H32 for tight bends. It normally needs a more generous inside radius and careful control of grain direction, tooling and edge quality.
Can aluminum sheet metal be laser cut?
Yes. Properly configured modern laser systems can cut aluminum sheet accurately. Process selection depends on alloy, thickness, feature size, edge requirements and production quantity.
Is aluminum sheet metal easy to weld?
Many aluminum alloys are weldable, but cleaning, filler selection, heat input and distortion control are important. Heat-treated alloys may lose strength near the weld, so the joint design must reflect the service load.
Should an aluminum drawing use gauge or millimeters?
Specify the alloy, temper and nominal thickness in inches or millimeters. Gauge can be shown as a reference, but numerical thickness prevents confusion with steel and stainless steel gauge systems.
What files are needed for an aluminum fabrication quote?
Provide a STEP or other 3D CAD file, a PDF drawing with critical tolerances, material and finish specifications, required quantity and delivery expectations. Include hardware, welding and inspection notes when applicable.
Request an Aluminum Sheet Metal Fabrication Review
Send your CAD model and drawing to Xproto for a project-specific review of alloy, thickness, bends, welding, finish, tolerances, quantity and delivery requirements.
Reference Notes
Alloy and temper terminology should follow the applicable material documentation. Useful primary references include the Aluminum Association standards program, Aluminum Standards and Data 2024, and ASTM B209/B209M for aluminum and aluminum-alloy sheet and plate. Final material, process and tolerance decisions must be confirmed against the project drawing, supplier certification and applicable specification.